
When a roll-to-roll UV DTF (ultraviolet direct-to-film) crystal transfer fails to release cleanly from the A-film backing or leaves fine letters stuck to the B-film carrier during application, the root cause almost always lies in an imbalance between UV varnish curing state, inline lamination roller temperature/pressure, and carrier peeling angle rather than defective ink alone.
For commercial print shops producing intricate brand emblems, showroom sample labels, and rigid packaging decals, mastering the mechanical interplay between A-film release coating and B-film carrier tack prevents costly gang-sheet waste.
How the A-Film and B-Film Differential Tack Mechanism Works
A roll-to-roll UV DTF transfer succeeds only when three adhesive interfaces obey a strict strength hierarchy. First, the cured ink stack (adhesive/white/CMYK/varnish) must bond more strongly to the clear B-film carrier than to the silicone-release A-film backing so that stripping the A-film lifts every letter cleanly onto the carrier. Second, once the decal is pressed onto a rigid object, the bottom pressure-sensitive adhesive must grip the target substrate more strongly than the top B-film grips the varnish layer.
When any part of that hierarchy drifts out of calibration, three classic shop-floor defects appear:
- A-film release failure (characters stay behind on A-film): If the top varnish layer is over-cured to a glass-hard, brittle finish before reaching the laminating nip roller—or if the nip roller pressure is too light—the B-film cannot wet out the top of small punctuation marks and thin strokes.
- Silvering and micro-bubbles along raised ink edges: Insufficient roller heat or uneven nip pressure traps microscopic air pockets around the vertical walls of high-build white and varnish ink layers.
- B-film refusal to release on the final product: Using an overly aggressive high-tack B-film or failing to degrease the rigid substrate causes fine graphics to lift right back off the product when the operator pulls the carrier sheet away.
Troubleshooting Matrix for Roll-to-Roll UV DTF Film and Peeling Defects
Operators can diagnose and correct most UV DTF transfer failures within a single test strip by matching the visible defect to its mechanical or curing variable.
| Observed Shop-Floor Defect | Primary Technical Cause | Immediate Corrective Action on the Line | Prevention Standard |
|---|---|---|---|
| Fine letters remain on A-film when stripping backing | Top varnish over-cured/brittle before lamination, or insufficient nip roller pressure | Check inline laminator roller pressure and mild pre-heat setting; peel A-film away from B-film on a flat table rather than pulling B-film upward | Keep minimum stroke thickness and adhesive underbase coverage within RIP choke limits |
| Cloudy “silvering” halo around raised emblem edges | Cold lamination or trapped air along thick white/varnish sidewalls | Enable moderate lamination roller warmth (per film manufacturer spec) and slow down take-up tension | Store A/B film rolls in a climate-stabilised room away from cold floor drafts |
| Adhesive halo or glue stringing outside graphic contour | Excessive printhead gap causing ink mist, or incompatible A-film coating batch | Lower printhead carriage gap to the standard film clearance and clean encoder/carriage base | Verify white-ink and varnish registration so ink seals the adhesive footprint cleanly |
| Graphic lifts back up with B-film on the rigid product | Substrate oil contamination or operator pulling B-film upward at 90 degrees | Degrease substrate with isopropyl alcohol (IPA), burnish firmly with a felt squeegee, and peel B-film back at a flat 180-degree fold | Allow 1–2 minutes of post-burnish dwell on cold glass or metal before stripping B-film |
Setting Artwork Choke and Minimum Stroke Rules Before RIP Output

Even perfect lamination cannot rescue artwork that lacks an adequate adhesive and white-ink foundation. Because the bottom adhesive and white layers provide the physical footprint that bonds a UV DTF crystal label to hard goods, floating hairline vectors or isolated 0.3 mm dots carry almost zero surface contact area.
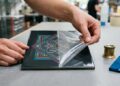
Pre-press operators should enforce a practical pre-flight checklist: maintain a sensible minimum stroke width for standalone text, apply a slight white-ink choke inside the CMYK layer so white edges do not peek out, and connect tiny floating punctuation marks with a clear varnish bridge when the client’s design permits. When stripping the A-film backing prior to application, always lay the transfer face-down and peel the flexible A-film away from the stiffer B-film carrier at a low angle.
Choosing Roll-to-Roll UV DTF Printers With Integrated Heated Lamination
Because A/B film separation and lamination tension directly determine transfer yield, commercial print shops benefit from roll-to-roll hardware that integrates printing, UV LED curing, and temperature-controlled lamination on a single rigid frame. Production managers evaluating compact 42 cm industrial roll-to-roll systems such as the XINFLYING XF-420S—or comparing wider production units like the XF-450S and XF-600S—can inspect the full range of XINFLYING roll-to-roll UV DTF printers to match media width and inline laminator controls to their shop’s daily transfer volume.
Running a rigid, inline-laminating platform like the XINFLYING XF-420S alongside climate-controlled film storage and flat-angle peeling discipline turns finicky fine-text crystal labels into a predictable, low-scrap production process.